Zirconia Oxygen Analyzer
Description
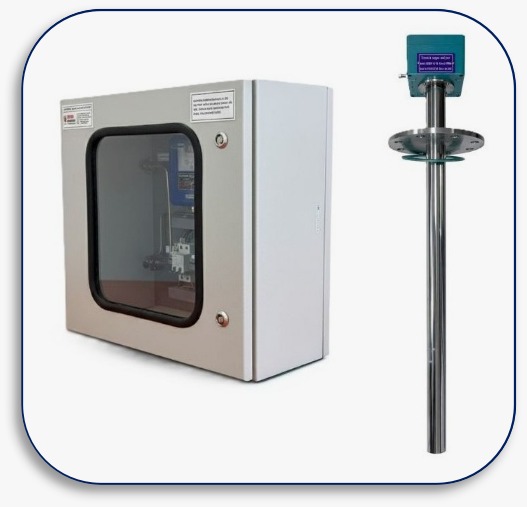
Combustion Efficiency Analyzers are designed to monitor oxygen levels and flue gas characteristics in real time to ensure optimal combustion performance. These systems help industries reduce fuel consumption, minimize emissions and improve overall boiler and furnace efficiency. With advanced zirconia-based sensing technology, the analyzers provide fast, accurate, and stable measurements even in high-temperature and harsh process environments. They are widely used in power plants, process industries, and various combustion-based applications for continuous optimization and regulatory compliance.
The products covered under Combustion Efficiency Analyzer include a range of advanced zirconia-based oxygen measurement solutions such as the Model ZGF-500 Zirconia Oxygen Analyzer, Model 7873 Zirconia Oxygen Analyzer, Model 6801 Zirconia Probe, and the Model M7873 Zirconium Oxide Oxygen Analyzer, along with the Oxy pink analyzer. These models collectively support precise and continuous oxygen monitoring for enhanced combustion efficiency.
Dosing system
Description
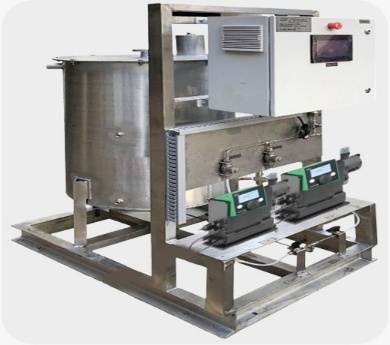
A dosing system is a water treatment solution designed to automatically maintain the correct pH and chlorine levels in various water systems such as swimming pools, cooling towers, wastewater treatment plants, and drinking water facilities. The system continuously monitors water quality using a pH sensor and controller, which adjusts the pH by dosing acid or alkali as required, and a chlorine (hypochlorite) sensor and controller that regulates sodium hypochlorite dosing to ensure effective disinfection. Dosing pumps accurately inject the required chemicals into the water stream, while a mixing chamber ensures proper dispersion for uniform treatment. Advanced dosing systems may also include data logging and remote monitoring capabilities, allowing real-time supervision and improved operational control
Digital Ph/ORP Senor
Features
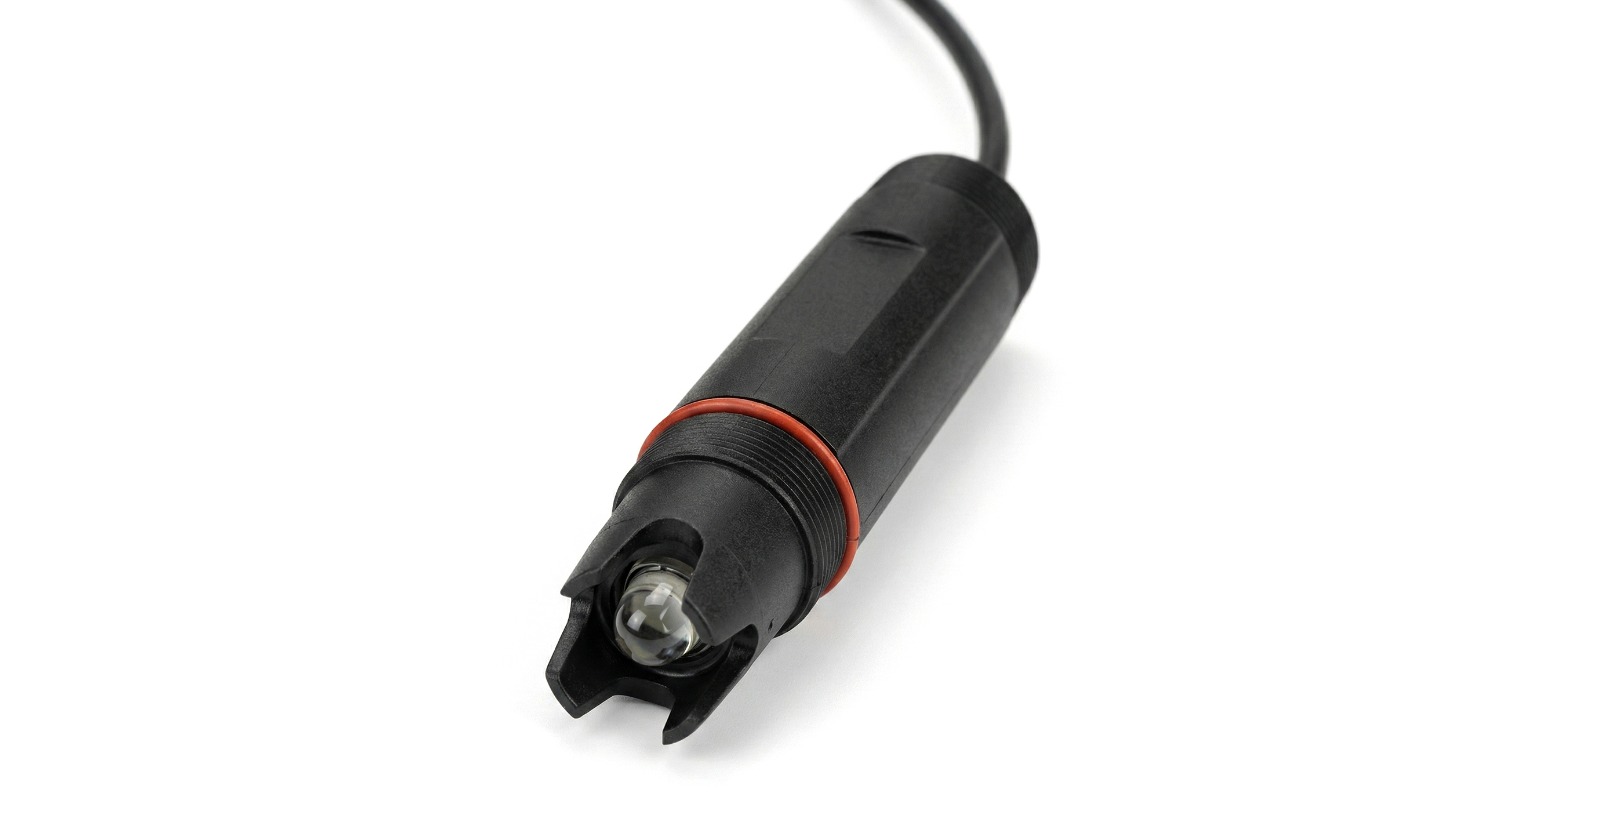
• Compact all-in-one design
• Support handheld devices and in-situ applications
• Large capacity reference, long service life
• 1 inch NPT mounting thread for flexible installation
• Internal storage of calibration data
• Support offline calibration, on-site plug and play
• Optional cleaning connector for underwater cleaning
• Standard Modbus protocol, support access to standard industrial control system
Specifications:
| Specification | Details |
|---|---|
Digital TSS/Turbidity Sensor
Features
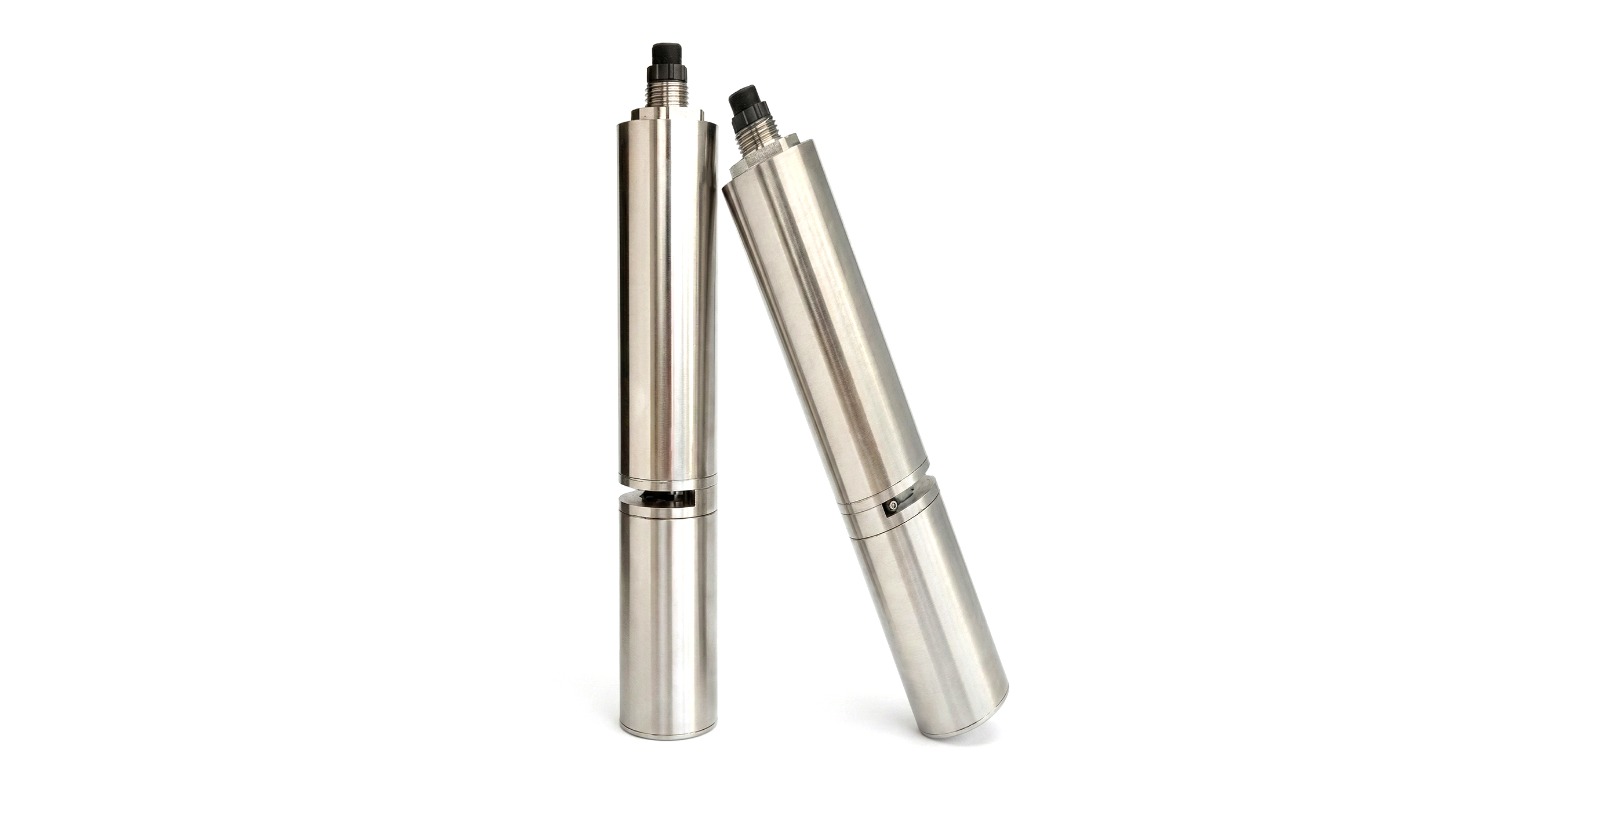
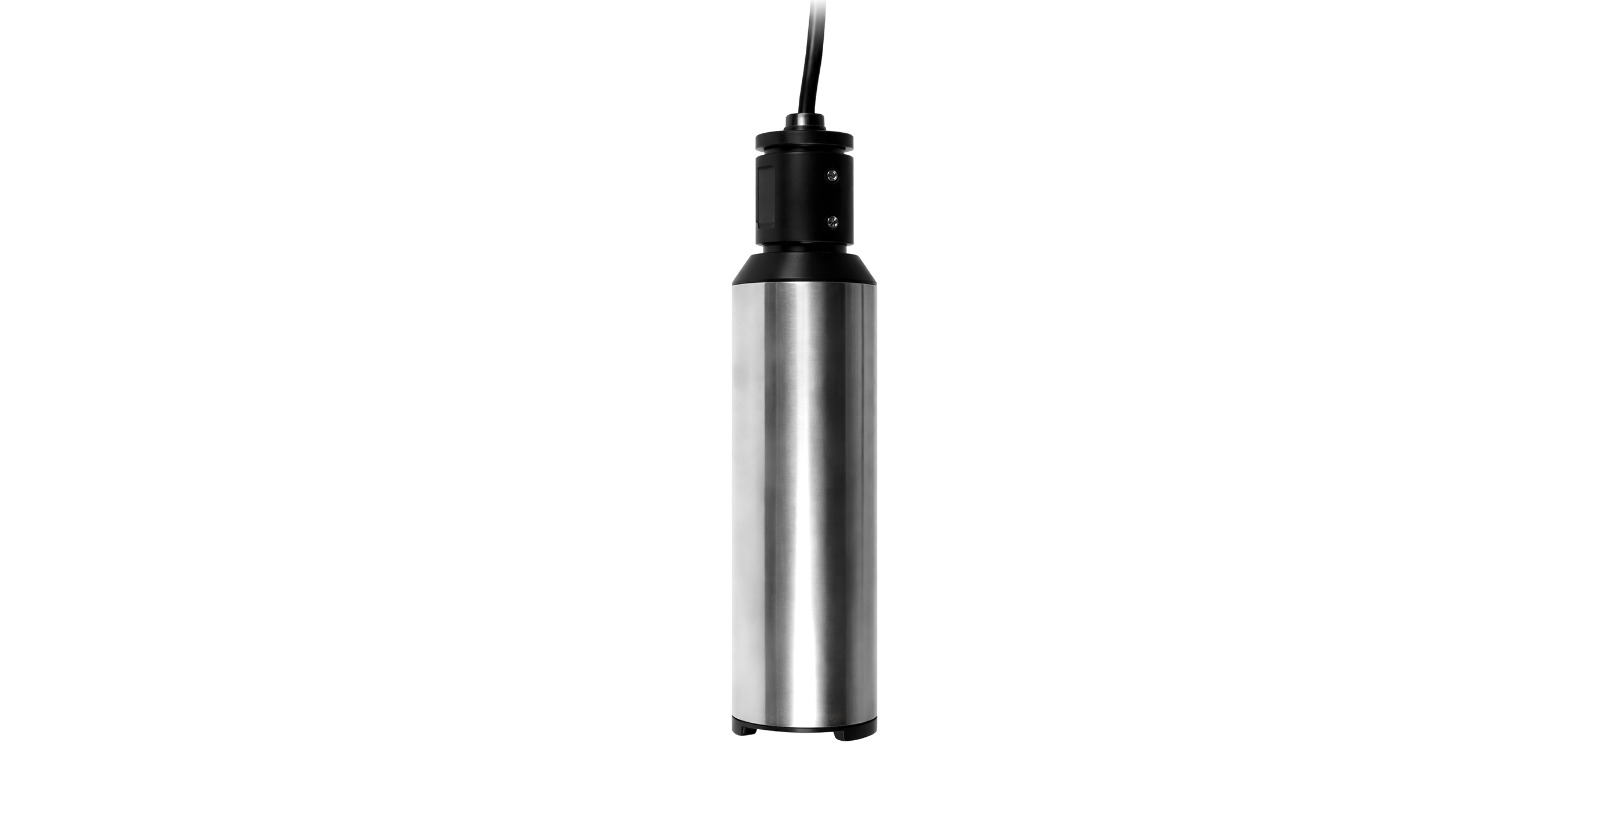
• Based on the infrared absorption and scattering light method
• Use ISO7027 method to continuously and accurately determine turbidity and suspended solids in water
• LED infrared scattering light source (850nm), stable wavelength, stable data
• Reliable performance, simple installation and calibration
• Self-diagnostic function, built-in humidity sensor and a light source detector
• Internal storage of calibration data, support offline calibration, plug and play
• Standard Modbus protocol, support access to standard industrial control system
Specifications:
| Specification | Details |
|---|---|
Digital COD Sensor
Description
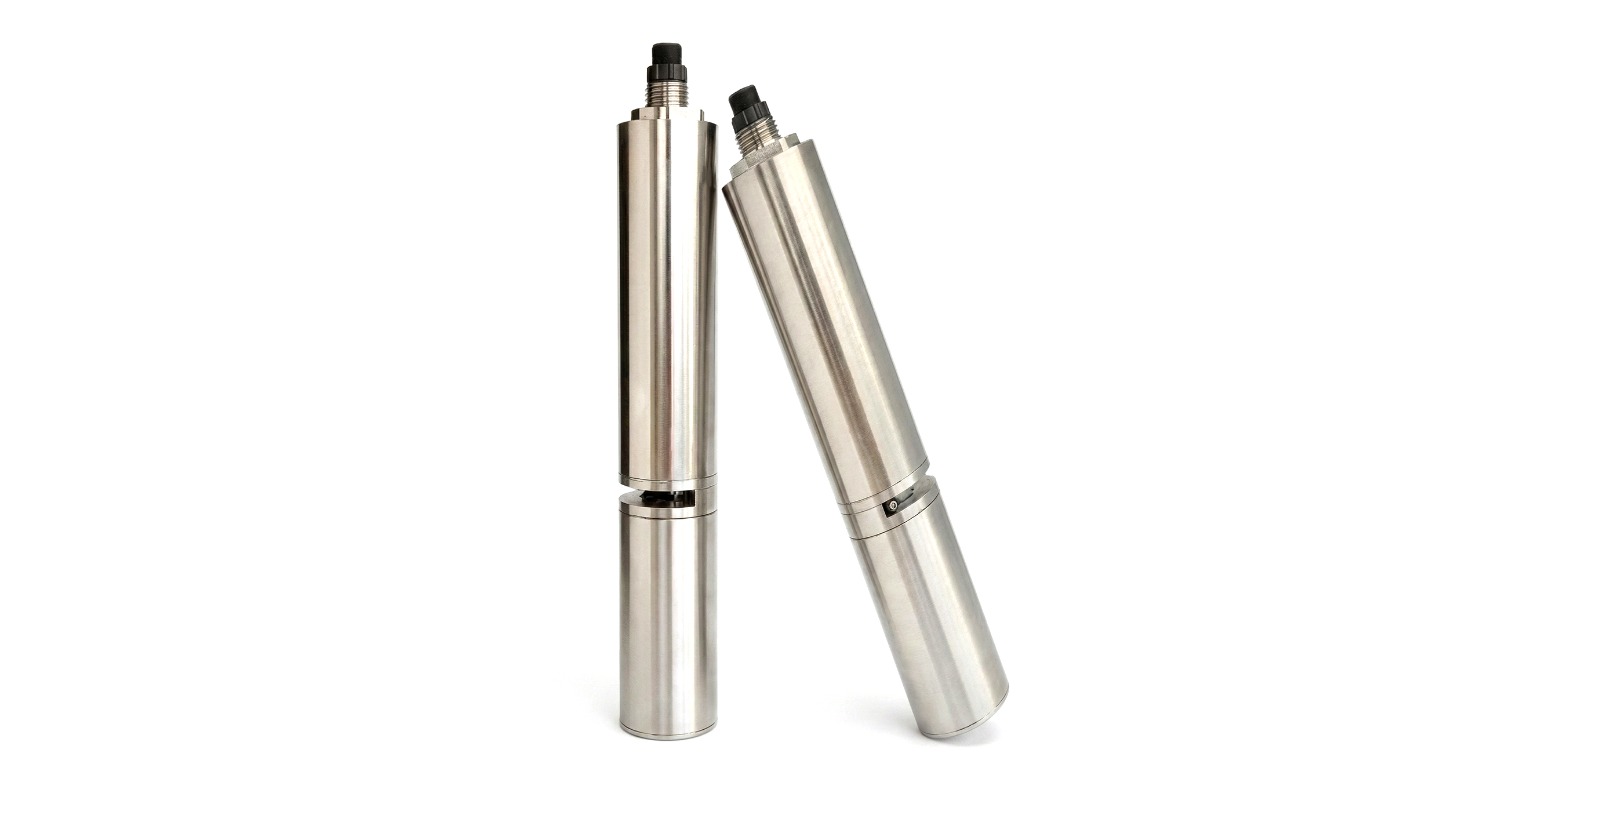
The total amount of organic pollutants in the water can be measured by measuring the degree of absorption of these organic substances to 254nmwavelength ultraviolet light.
The COD 351 digital sensor adopts two light sources, one 254nm ultraviolet light, and one turbidity compensation, which can automatically eliminate the interference of suspended substances in the water, so as to achieve more stable and reliable measurement.
Features
• RS-485 output, support Modbus
• No reagents, no pollution, environmentally friendly
• Can measure COD, TOC, turbidity and temperature
• Automatically compensate for turbidity interference
• With self-cleaning brush and the maintenance cycle is longer
Specifications:
| Specification | Details |
|---|---|
Effluent Quality Monitoring System (EQMS)
Description
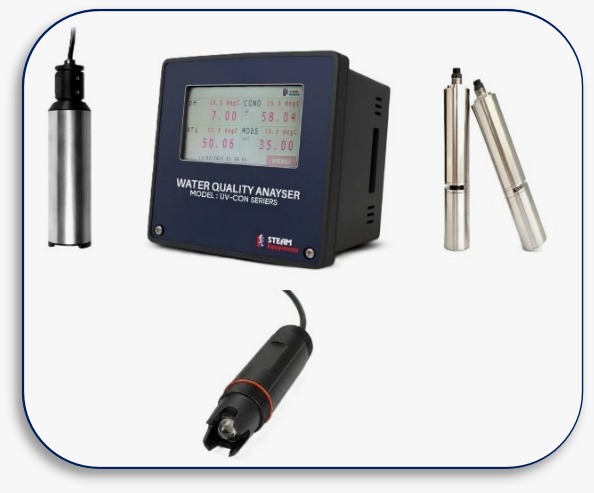
An Effluent Quality Monitoring System (EQMS) is designed for the continuous and accurate monitoring of wastewater discharge from industrial processes. The system measures key parameters such as pH, COD, BOD, TSS, TDS, dissolved oxygen, conductivity and flow to ensure compliance with CPCB and local pollution control board norms. EQMS provides real-time data transmission, remote monitoring capability, and reliable performance in harsh environmental conditions. It helps industries maintain transparency, improve treatment efficiency and ensure safe and environmentally responsible effluent disposal.
Features
Specifications:
| Specification | Details |
|---|---|
Dust Analyser (Opacity Monitor)
Description
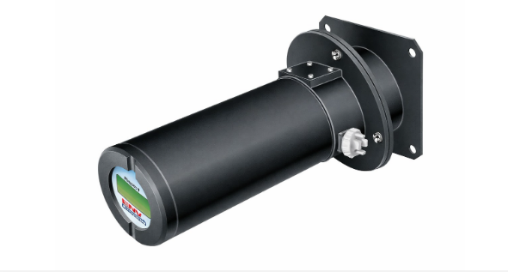
Online dust monitoring devices (also known as opacity monitors) are used for continuous monitoring of particulate matter concentration in industrial emissions. The system operates on the principle of laser back-scattered light and is designed to measure dust concentration from various emission sources. It can be integrated with Continuous Emission Monitoring Systems (CEMS) or connected to dust monitoring networks through a shared data acquisition and processing system. These devices are generally used for monitoring and control of soot and particulate emissions from power generation boilers, industrial furnaces and industrial boilers across industries such as thermal power, iron and steel, petrochemicals, chemicals, cement production, ceramics and waste incineration. The system typically comprises optical components, circuit and control sections, calibrator and purge system.
Products Covered: Back Scattering Dust Analyzer, Cross Duct Type and Tribo Electric Type.
Features
Specifications:
| Specification | Details |
|---|---|
Ambient Air Quality Monitoring System (AAQMS)
Description
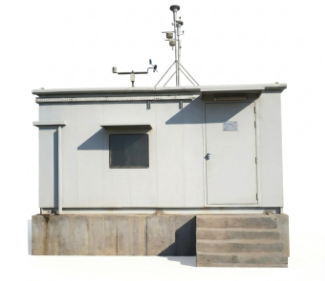
Ambient Air Quality Monitoring Systems (AAQMS) are automated systems used for continuous monitoring of ambient air quality in industrial, urban and environmentally sensitive areas. The system measures concentrations of key air pollutants such as PM₁₀, PM₂.₅, SO₂, NOx, CO, O₃ and NH₃, along with meteorological parameters including temperature, relative humidity, wind speed, wind direction, rainfall and atmospheric pressure. AAQMS typically comprises analyzers, sample collection and conditioning systems, calibration facilities and a data acquisition and handling system housed within a weatherproof analyzer shelter designed for outdoor operation. The system supports continuous data monitoring, recording and transmission for environmental monitoring
Features
Tribo Electric Type
Description
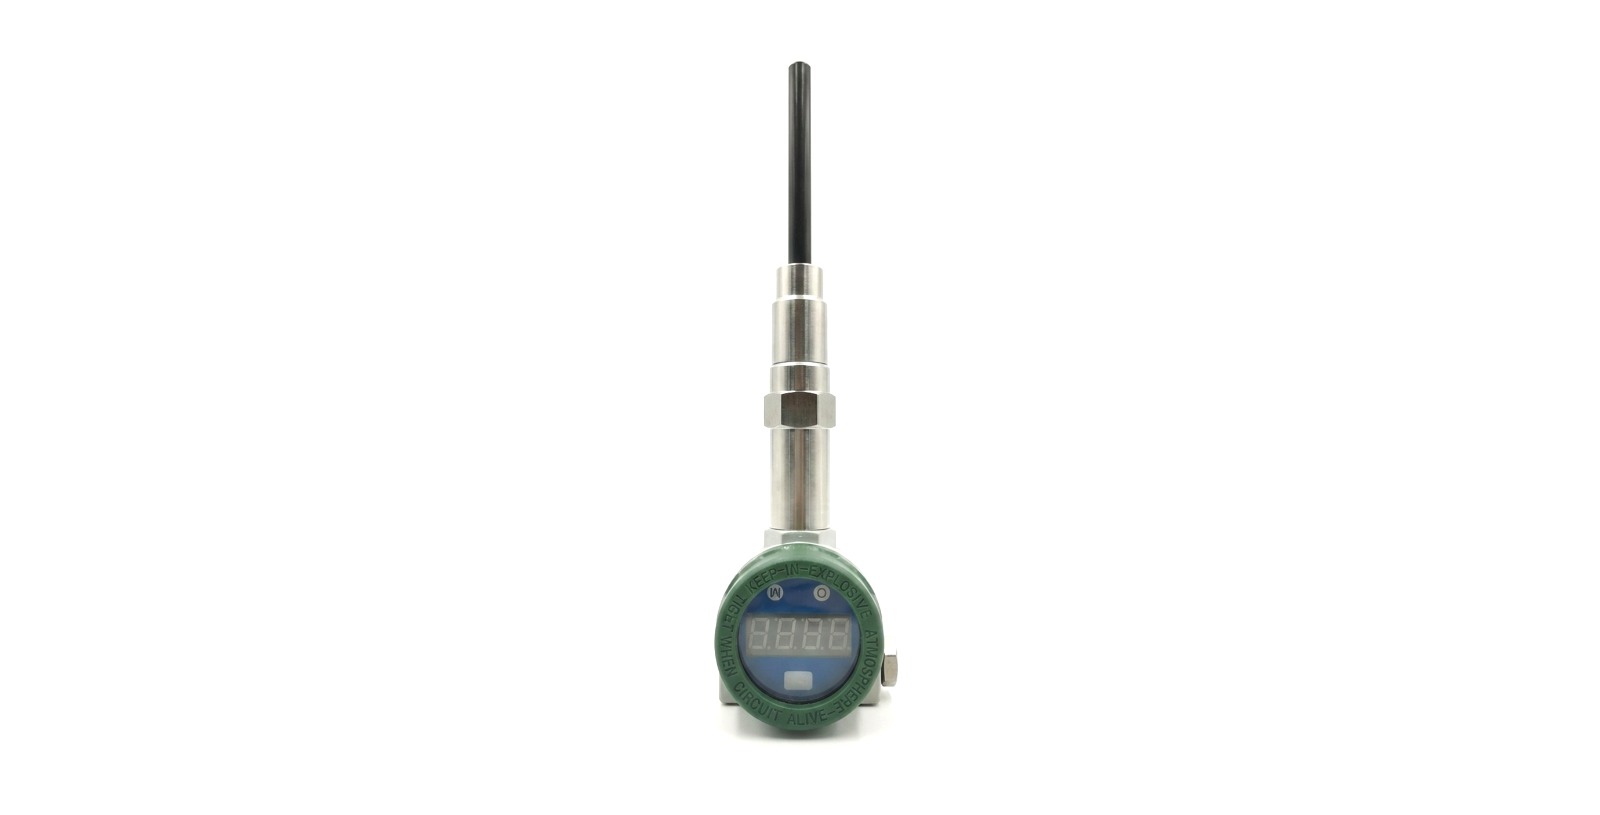
Dry dust detector adopts the world's most advanced principle of charge induction measurement, independently developed and produced by our company.The series of products are widely used in steel, metallurgy, power generation, petroleum, chemical, cement, mining and other industries gas solid two-phase flow dust concentration online measurement.Typical application: the blast furnace gas bag dust removal, TRT power generation, dry method and wet method, electrostatic dust removal, carbon concentration on-line continuous monitoring pulverized coal boiler, instead of in the past by artificial old timing sampling analysis, found that dust emission concentration in time, avoid the loss of available dust, protect gas recycle production equipment, lower consumption, deeply user welcome!
During the transportation of gas-solid two-phase fluid containing dust particles, dust particles will be charged due to the collision and friction between dust particles and dust particles and the inner wall of the pipe.When charged dust particles pass through the special measuring electrode, the measuring electrode can induce positive and negative electric charges, and the electric charges can form pA current signals in the transfer movement.The size of the ac signal is proportional to the dust mass.The dust concentration (mg/m3) can be accurately measured by further amplifying and processing the electrical signal.
Features
•. Dust concentration is measured by charge induction principle with high measurement accuracy.
•. Integrated structure, long distance of current signal transmission, strong anti-interference ability.
•. The measuring electrode is protected by spraying or casing, which improves the ability of high temperature resistance, corrosion resistance and adhesion resistance, reduces cleaning and maintenance, prolongs service life and improves product quality.
•. The main part of the sensor adopts patent design, and the air-tight connector strictly prevents the gas leakage under test and the measuring electrode is impacted out due to pressure, which guarantees the safety of the circuit and the staff.
•. Non-polar two wire connection, low power consumption operation, improve the safety of the product and field use.
•. Adopt full metal shell, waterproof, dustproof and explosion-proof.
Specifications:
| Specification | Details |
|---|---|
Cross Duct Type
Description
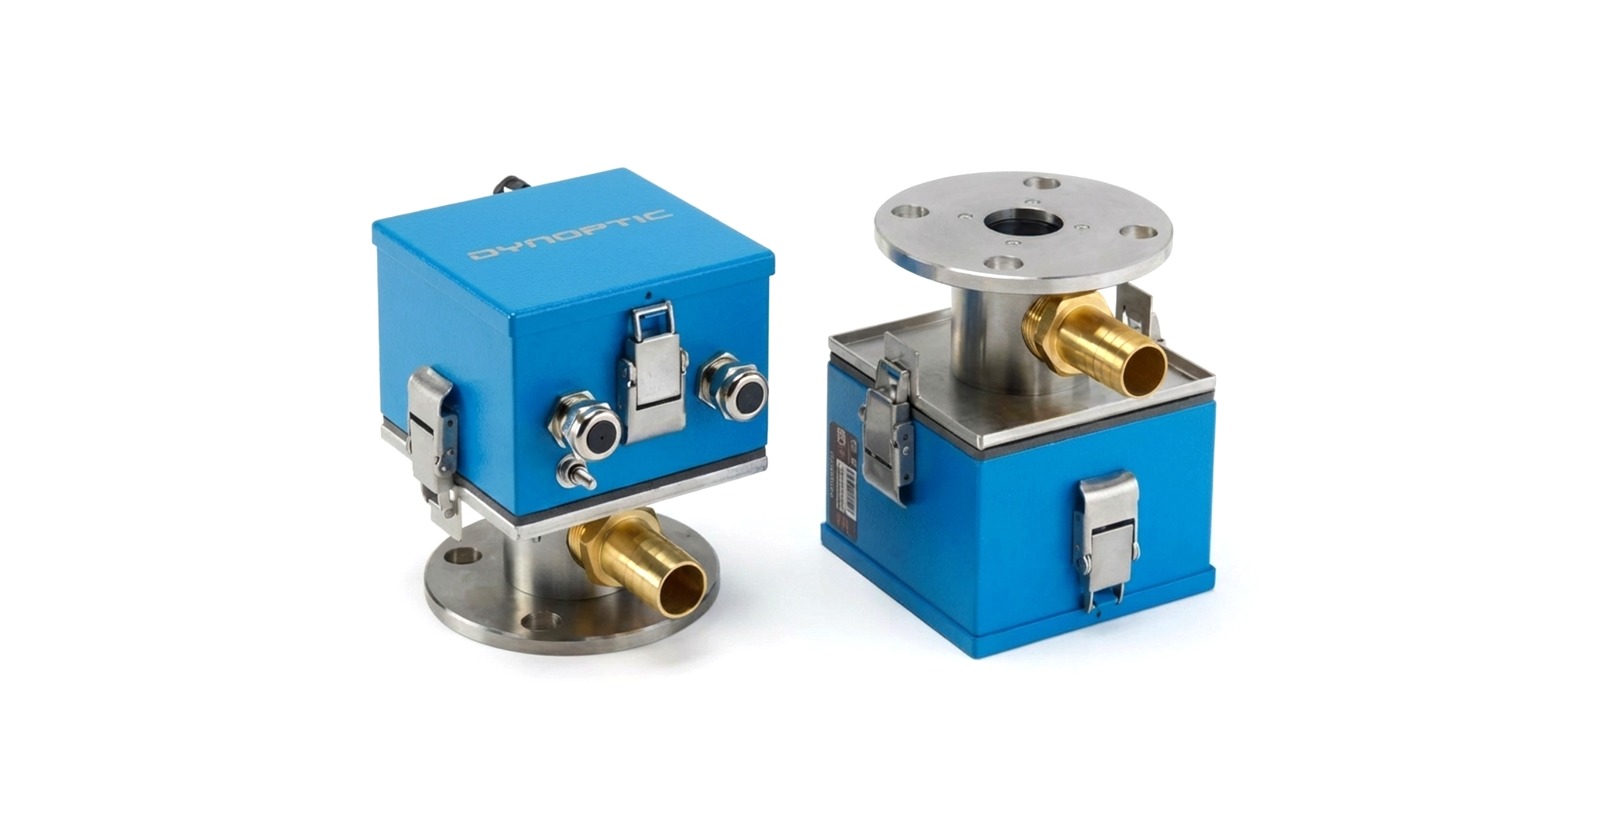
The DSL-340 is an optical instrument designed to measure the concentration of dust or particulate matter suspended in the exhaust gas passing through a duct, stack, or flue; typically, the exhaust gas from an industrial combustion process or air filtration system.
The DSL-340 uses the innovative Dynamic Detection Principle (DDP) which measures fluctuations in the intensity of a light beam, using a folded beam Transceiver / Reflector arrangement. Increased particulate density in the stack causes the amplitude of these fluctuations to increase. When calibrated against standard reference measurements, the amplitude of this signal relates directly to the particulate concentration in the stack, and this can be used to present as a reading in mg/m³.
Unlike the standard transmission technique, DDP has immunity to gradual reductions in the absolute intensity of the light signal and therefore, has the advantage that it is significantly less susceptible to drift with time, temperature or dirtying optics, than traditional opacity monitors using the standard transmission technique.
The light source in the Transceiver is a long life, stabilised green LED which offers long life and stable intensity. The transmitted light beam is pulsed to give complete immunity to ambient light levels. The intensity of the transmitted light is monitored at source so that any variations in the emitted light level are compensated in the received signal. The Transceiver has on board temperature measuring to provide stability over temperature.
The DSL-340 is available with or without an Operator Interface (control unit) so for the most cost effective monitoring solution the DSL-340 can operate as a “stand-alone” instrument consisting of the Transceiver head (TRX) and Reflector head, with all electrical connections (including outputs such as the alarm relays, 4-20mA and Modbus) being made inside the TRX head. As a stand-alone instrument the DSL-340 is set-up and controlled using the supplied utility software, installed on a PC or laptop, and connected via the USB connector on the TRX. When supplied with an Operator Interface (OI) all power supply and output connections are made in the OI rather than the TRX.
The DSL-340 has no moving parts, is of rugged design and has an excellent reliability record. Regular maintenance simply involves cleaning the optical surfaces which are easily accessible due to our latched head design. Both the TRX and Reflector heads are supplied with an air purge body, which when connected to a high volume source of clean air, keeps the contaminated stack gas away for the lens surfaces. An Aluminium air purge body is available for use on standard installations and a more advanced Stainless Steel air purge body is available for more demanding installations.
Features
• US EPA PS-11 compliant
• Dynamic Detection Principle (DDP) measurement technique results in increased immunity to drift
• Measurement reading as mg/m3 (when calibrated against standard reference measurements)
• Internal electronic calibration check facility
• Rugged 316L stainless steel construction
• Choice of interface options enabling easy integration
• Free utility software for PC based setup, control, and data logging
• Optional Operator Interface (OI) with different mounting configurations
Specifications:
| Specification | Details |
|---|---|
Online Extractive Flue Gas Analyzer
Description
A Continuous Emission Monitoring System (CEMS) is designed to measure and record real-time emissions from industrial stacks and flue gas outlets. These systems help industries comply with CPCB/PCB environmental norms by continuously tracking key pollutants such as SOx, NOx, CO, CO₂ and other critical emission parameters. CEMS ensures accurate monitoring, process optimization, and regulatory reporting through reliable sensors, advanced data acquisition systems, and long-term stable performance even in harsh industrial conditions.
The products covered under CEMS include a range of advanced gas monitoring solutions such as IN-SITU Type Flue Gas Analyzers for SOx, NOx, CO, and CO₂ measurement, high-precision IN-SITU Laser Gas Analyzers, dedicated CO Analyzers, and Extractive Type CEMS for detailed sample-based analysis. The portfolio also includes Hot Wet Extractive Systems designed for high-moisture flue gases, along with the IM–TPF 100 model for stable and continuous industrial emission monitoring.
Features
Specifications:
| Specification | Details |
|---|---|
Online In-situ Type Flue Gas Analyzer
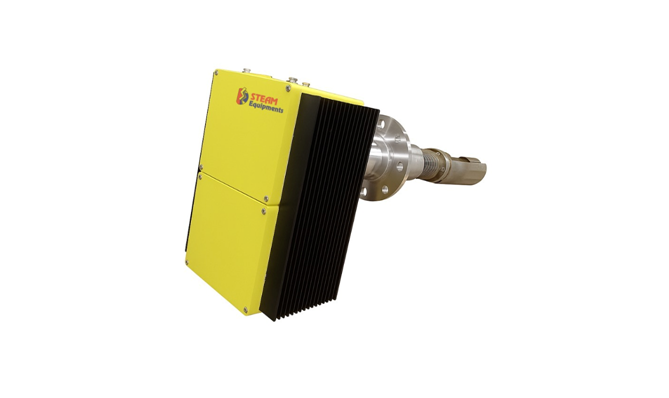
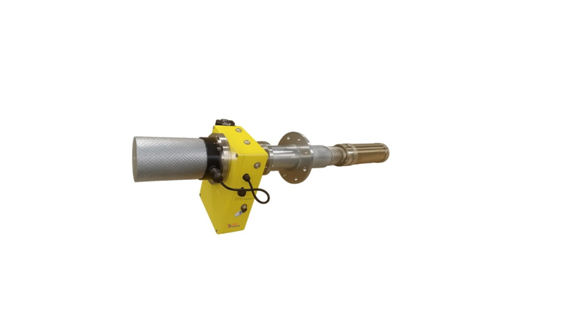
Description
Model: UT-IN-S-N-O-H-230
SO2-NO2-CO2 measurement:
• This analyzer uses UV absorption (for SO₂ and NO₂) and IR spectroscopy (for CO₂) in a compact, robust sensing head with LED light sources and no moving parts, requiring virtually zero maintenance.
Accuracy is ensured through automatic zero calibration using ambient air, with CO₂ scrubbed by a long-life disposable filter (2+ years replacement interval).
• Service needs are minimal: 36V DC power (@50 VA) and RS485 digital output via a single 4-way sealed connector.
NO/H2O Measurement:
• The NO/H₂O sensor uses the same in-situ probe design as the SO₂/NO₂/CO₂ sensor but employs a Quantum Cascade Laser (QCL) as the radiation source. The QCL provides a narrow, precise IR beam, allowing measurement of a single NO absorption line free from H₂O interference for highly accurate, noise-free readings. It simultaneously measures H₂O concentration using a nearby spectral line.
• Unlike traditional chemiluminescence (maintenance-heavy) or IR/UV methods (cross-sensitivity and short lamp life issues), the QCL offers long-term stability, no moving parts, and virtually zero maintenance, with a lifetime measured in decades.
• The analyzer measures NO from <10 ppm to several thousand ppm at temperatures up to 450 °C and can be adapted for other gases (e.g., NH₃) by selecting a suitable QCL wavelength, making it ideal for applications like SCR control in coal-fired power plants.
Features
• INSITU CEMS suitable for Refineries, power plant & other industries.
• Measurement gas resolution 1 PPM and accuracy +/-2% of reading
• UV absorption spectroscopy based SO2 & NO2 measurement, Laser (QCL) based NO & H2O measurement and Infrared spectroscopy-based CO2 measurement
• Remote monitoring of system available.
• Simple Installation as per the photograph
• Light weight so easy to installation.
• Low maintenance cost
• No Shelter required
Specifications:
| Specification | Details |
|---|---|
Online In-situ Ex Type Flue Gas Analyzer
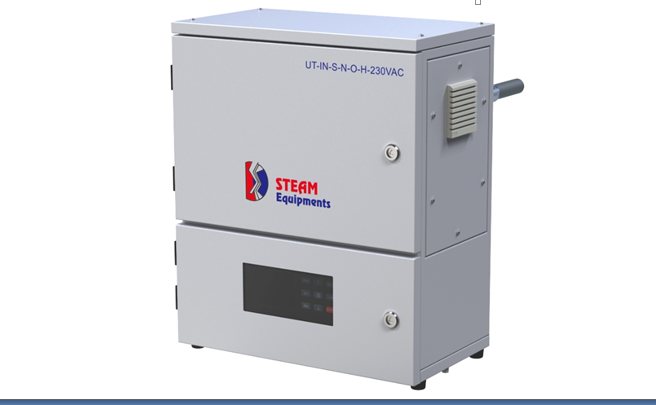
Description
Model: UT-IN-S-N-O-H-230VAC
UT-IN series Flue Gas Analyzer is a highly integrated single-flange gas monitoring equipment, of which, core detection module adopts Tunable Diode Laser Absorption Spectroscopy (TDLAS), Differential Optical Absorption Spectroscopy (DOAS) gas absorption technology and Zirconia with independent intellectual property rights. The specially designed measuring cell effectively improves optical path length for gas absorption, which can measure trace gas accurately inside pipeline UT-IN series can be widely applied in online gas monitoring occasions including denitrification device, boiler flue and exhaust detection, etc. One equipment can realize online monitoring for multiple gas components, such as CO, CO2, SO2, NO, NO2, O2, H2O etc.
Features
• Adopt single-flange design with high integration
• and easy installation
• Measurement gas resolution 1 PPM and accuracy +/-2% of fs
• Remote monitoring of system available.
• Simple Installation as per the photograph
• With high-temperature flowmeter, user can
• observe flow during equipment operation
• Low maintenance cost
• Sampling measurement is free from interference of pipeline deformation, high dust and other working condition change, with strong adaptability
• No Shelter required
Specifications:
| Specification | Details |
|---|---|